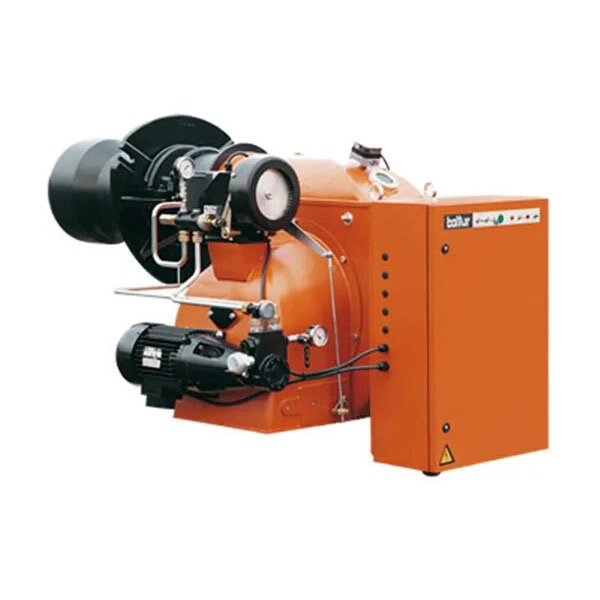
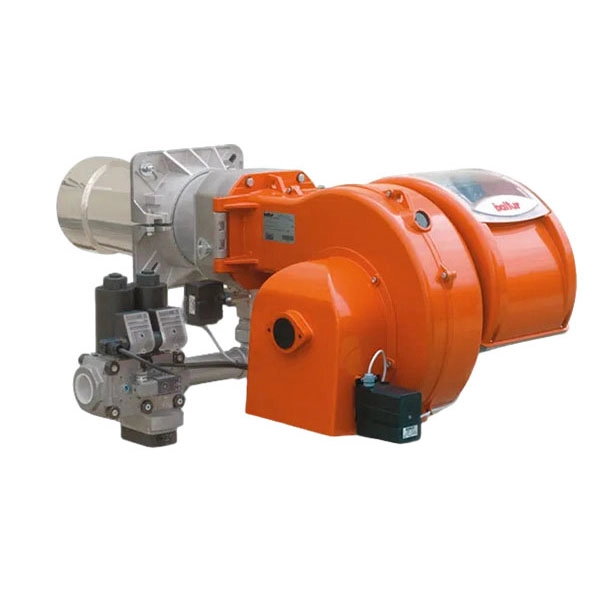
Cold start issues in large industrial burners present a persistent challenge for operators, often leading to delayed ignition, incomplete combustion, increased emissions, and accelerated equipment wear. When a burner is started from ambient temperature, the fuel-air mixture may fail to reach autoignition conditions, resulting in misfires or hazardous accumulation of unburned fuel. Addressing these problems requires a systematic approach to preheating — a set of strategies designed to raise the temperature of combustion air, fuel, and burner components before ignition. This article explores the root causes of cold start difficulties and presents proven preheating methods, with a focus on practical implementations that enhance reliability, safety, and efficiency. As an experienced provider of combustion solutions, SHUXIN has developed integrated preheating systems that help industrial facilities overcome these challenges while maintaining operational flexibility.
Understanding the Root Causes of Cold Start Failure
Cold start problems stem from the fundamental thermodynamics of combustion. At low temperatures, fuel vaporization slows down, the air-fuel mixture becomes less homogeneous, and the flame propagation speed decreases. For large industrial burners, these effects are magnified due to the high thermal mass of the combustion chamber and the long fuel supply lines. Common failure modes include:
- Flame instability: The flame may extinguish shortly after ignition if the heat release rate is insufficient to sustain combustion.
- Smoking and soot formation: Incomplete combustion at low temperature produces carbon particles that foul heat exchanger surfaces.
- Thermal shock: Rapid introduction of hot flame into a cold burner body can cause differential expansion, cracking refractory linings.
Without proper preheating, operators often resort to prolonged purge cycles or multiple ignition attempts, which waste fuel and time. Therefore, a structured preheating strategy is not merely an optimization — it is a prerequisite for safe and reliable burner operation.
Preheating Strategies: From Simple to Advanced
Depending on burner design, fuel type, and operating requirements, preheating can be implemented at various points in the system. The following sections describe the most effective approaches.
1. Combustion Air Preheating
Raising the temperature of the incoming combustion air is one of the most direct methods to improve cold start performance. By using a heat exchanger that recovers waste heat from the flue gas, or integrating an electric or steam air heater, the air temperature can be elevated to 150–300 °C before mixing with fuel. This significantly lowers the activation energy required for ignition. SHUXIN's air preheaters are designed with high-efficiency finned tubes that minimize pressure drop while maximizing heat transfer, ensuring stable air temperatures even during variable load conditions.
2. Fuel Preheating Systems
For liquid fuels such as heavy fuel oil or biodiesel, viscosity drops sharply with temperature. Preheating the fuel to the optimal viscosity range (typically 100–150 °C for heavy oil) ensures proper atomization and mixing. Gas fuels, on the other hand, benefit from preheating to prevent condensation of heavier hydrocarbons. SHUXIN offers fuel preheating stations that incorporate temperature-controlled electric heaters or steam heaters, with redundant safety interlocks to prevent overheating. These systems can be retrofitted to existing burner trains without major modifications.
3. Burner Block and Refractory Preheating
The thermal mass of the burner itself — including the burner block, nozzle, and refractory lining — acts as a heat sink during startup. Preheating these components using a small pilot flame or an external hot air blower brings them to a temperature near the ignition threshold. SHUXIN recommends a staged preheat sequence: first circulate hot air through the burner throat for 5–10 minutes, then introduce a low-fire pilot flame before ramping up to full load. This method reduces thermal stress and extends the service life of the burner tile.
Implementing a Preheating Strategy: Practical Considerations
Every industrial site has unique constraints. When selecting a preheating approach, facility engineers should evaluate the following factors:
- Fuel type and availability of waste heat sources
- Burner turndown ratio and minimum firing rate
- Ambient temperature variations across seasons
- Existing control system capabilities
The most robust solution often combines two or more strategies. For example, SHUXIN has implemented systems for steel reheating furnaces where combustion air is preheated by a flue gas recuperator while a small electric heater maintains fuel temperature during standby. This hybrid approach ensures rapid cold start even in subzero climates, reducing startup time from over 30 minutes to less than 12 minutes in field trials.
Conclusion: Elevating Cold Start Reliability with SHUXIN Expertise
Cold start issues in large industrial burners are not unavoidable. By adopting a systematic preheating strategy tailored to the specific fuel and equipment configuration, operators can eliminate ignition failures, reduce emissions, and improve overall plant uptime. SHUXIN brings decades of combustion engineering experience to help clients diagnose cold start problems and deploy cost-effective preheating solutions — from standalone air heaters to fully integrated turnkey systems. Whether you are designing a new burner system or retrofitting an existing one, investing in preheating capability pays dividends in safety, reliability, and energy efficiency. Contact SHUXIN to discuss your burner's cold start performance and discover how our preheating strategies can transform your operations.
 English